1, Environmental adaptability: a dual test of corrosion resistance and explosion-proof design
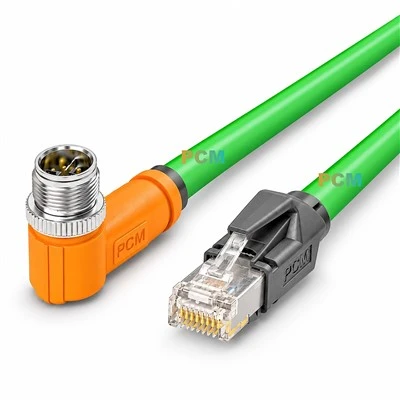
In the chemical industry, M12 adapters need to be exposed to corrosive media such as acid, alkali, salt spray, and organic solvents for a long time, and their shell materials and sealing structures need to meet strict corrosion resistance requirements. For example, a petrochemical company experienced internal circuit short circuit and equipment shutdown due to the brittleness of the outer shell and aging of the sealing ring of an M12 adapter with a regular plastic shell within 3 months. Industry practice has shown that chemical plants should prioritize the following configurations:
Material upgrade: Adopting 316L stainless steel or special alloy shell, its corrosion resistance is more than three times higher than ordinary stainless steel, and it can resist strong corrosive gases such as chloride ions and hydrogen sulfide.
Sealing enhancement: equipped with double-layer silicone O-rings and IP69K protection level, ensuring that the sealing performance can still be maintained in a high-temperature steam flushing environment of 100 ℃. A certain chemical plant has extended the equipment maintenance cycle from 3 months to 2 years by upgrading the sealing structure.
Explosion proof certification: In flammable and explosive areas such as tank storage areas and reaction kettle surroundings, Ex d explosion-proof adapters certified by ATEX or IECEx must be selected, with a shell thickness of ≥ 3mm and equipped with spark suppression devices to prevent internal arcs from igniting external gases.
2, Electrical performance: dynamic current management and signal integrity assurance
The starting current of chemical equipment (such as flow meters and pressure sensors) may reach 3-5 times the rated value. If the adapter selection is improper, it can easily cause problems such as overheating and a surge in contact resistance. A certain chemical plant stopped production for 12 hours due to the use of an M12 adapter with a rated current of 4A to drive a pump with a starting current of 8A, resulting in welding of the adapter contacts. The key response measures include:
Reduced rating design: Select based on 80% of the actual working current, for example, when driving 5A equipment, choose an adapter with a rated current of 6.3A.
Dynamic compensation technology: using an intelligent adapter with integrated PTC thermistor, the circuit is automatically cut off when the current exceeds the threshold, and power is restored after the temperature drops to a safe range. After a certain enterprise applied this technology, the adapter failure rate decreased by 75%.
Signal shielding optimization: For adapters that transmit 4-20mA analog signals or industrial Ethernet signals, a tin plated copper braided shielding layer with a shielding effectiveness of ≥ 60dB is required to suppress electromagnetic interference. A certain chemical plant upgraded its shielding structure and reduced the data packet loss rate from 15% to 0.5%.
3, Mechanical protection: structural reinforcement for vibration and impact resistance
The vibration generated during the operation of chemical equipment (frequency 5-200Hz, acceleration ≤ 5g) may cause the adapter pins to loosen or the casing to crack. Due to the lack of reinforcement for M12 adapters in vibration environments, 30% of the adapters in a certain synthetic ammonia factory experienced poor contact within 6 months. Industry solutions include:
Upgrading of locking mechanism: The hexagonal circular arc locking outer ring is selected, which has a 40% increase in torque bearing capacity compared to traditional designs and can resist high-frequency vibrations. After being applied by a certain enterprise, the adapter looseness rate decreased from 12% to 0.3%.
Plug and unplug lifespan test: The adapter is required to pass over 500 plug and unplug cycles to ensure reliability in frequent maintenance scenarios. In a simulated chemical scenario test, the contact resistance of a certain brand adapter only increased by 0.2m Ω after 1000 insertions and removals.
Cable fixing scheme: Stainless steel cable clamps and anti drop nuts are used to prevent the cable from detaching from the adapter due to vibration or external pulling. A certain chemical plant reduced the damage rate of adapters by 80% by standardizing cable fixation.
4, Installation specifications: closed-loop management of standardized operation and regular maintenance
The installation quality of M12 adapters in chemical plants directly affects their service life. A certain enterprise caused a water ingress fault in the adapter within one month due to failure to comply with installation specifications, resulting in a direct economic loss of 200000 yuan. The key installation points include:
Environmental pre-treatment: Before installation, clean the installation surface with a dust-free cloth and wipe the adapter contacts with alcohol to remove oil stains and oxidation layers. A certain enterprise has reduced the failure rate of poor contact from 8% to 0.5% by standardizing the cleaning process.
Torque control: Use a torque wrench to tighten the adapter according to the standard value (usually 0.6-0.8N · m) to avoid loosening caused by cracking or loosening of the housing due to over tightening. A certain brand of adapter showed in torque testing that when the tightening torque exceeds 1.2N · m, the deformation rate of the shell reaches 15%.
Regular inspection: Establish a "daily inspection+weekly inspection+monthly inspection" system, focusing on inspecting the appearance of the adapter (whether there are cracks or corrosion), sealing (verified by an airtight detector), and electrical performance (measured by a multimeter for contact resistance). A certain chemical plant has identified and addressed 12 potential faults in advance by implementing this system.
5, Industry case: M12 adapter upgrade practice of a certain chemical group
A large chemical group discovered serious hidden dangers in corrosion, vibration, and current overload of the original M12 adapter during the intelligent transformation of its production equipment. The significant improvement in equipment operation stability and maintenance efficiency has been achieved through the following upgrade measures:
Material upgrade: Replace all adapter housings with 316L stainless steel and use gold-plated contacts (coating thickness ≥ 0.5 μ m), reducing contact resistance from 1.2m Ω to 0.3m Ω.
Structural optimization: Select an adapter with IP69K protection level and double-layer sealing ring, and integrate PTC overcurrent protection module, reducing the fault response time to 0.1 seconds.
Intelligent management: Deploy IoT sensors to monitor adapter temperature, vibration, and current data in real-time, predict fault risks through AI algorithms, and shift maintenance cycles from passive maintenance to proactive prevention.
After the upgrade, the comprehensive failure rate of the group's equipment decreased by 65%, and the annual maintenance cost decreased by 3 million yuan, verifying the key role of scientific selection and standardized management in the application of M12 adapters in chemical scenarios.